Define the pack
Start with bottle size, neck finish, trigger cap type, dip-tube length and filled weight.
Trigger Capping Line ROI UK
This guide is for commercial decision-makers comparing labour savings and production gains. It explains the practical trigger capping considerations that affect specification, quotation and performance after installation.
Buyer guidance
This page is aimed at commercial decision-makers comparing labour savings and production gains. The right machine route depends on the cap, bottle, dip tube, output target and the wider line rather than the machine name alone.
Specification priorities
These points help narrow the shortlist before samples are reviewed or a formal quotation is prepared.
Start with bottle size, neck finish, trigger cap type, dip-tube length and filled weight.
Compare required bottles per minute, shift pattern, batch size and operator availability.
Include installation, commissioning, operator handover, spares and practical aftercare in the project scope.
Related machinery
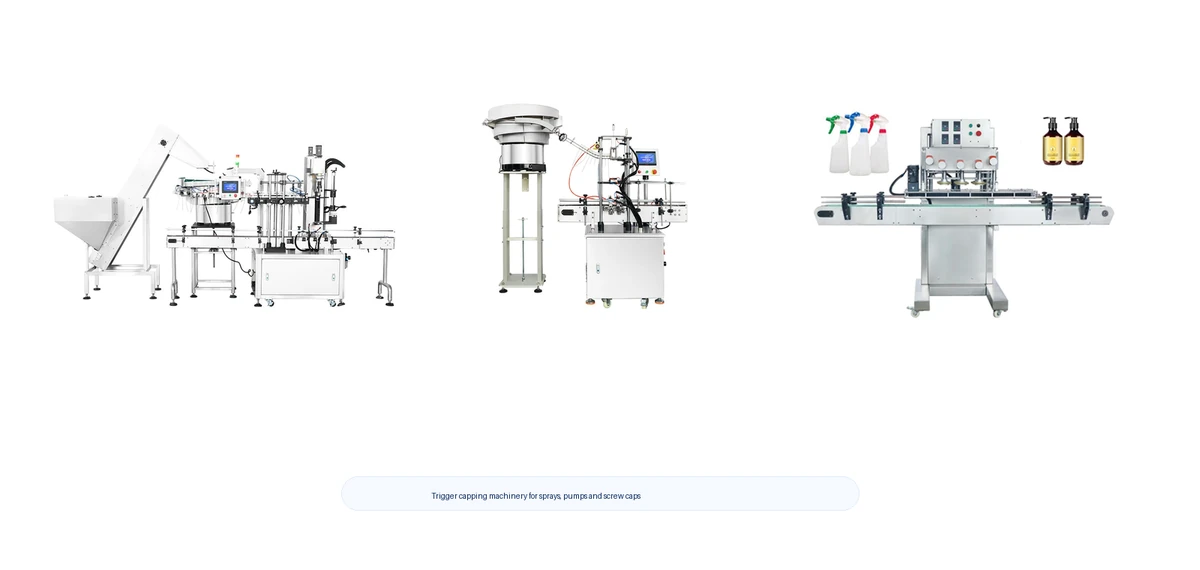
Use these machine routes to compare the practical equipment options before sending samples for review.
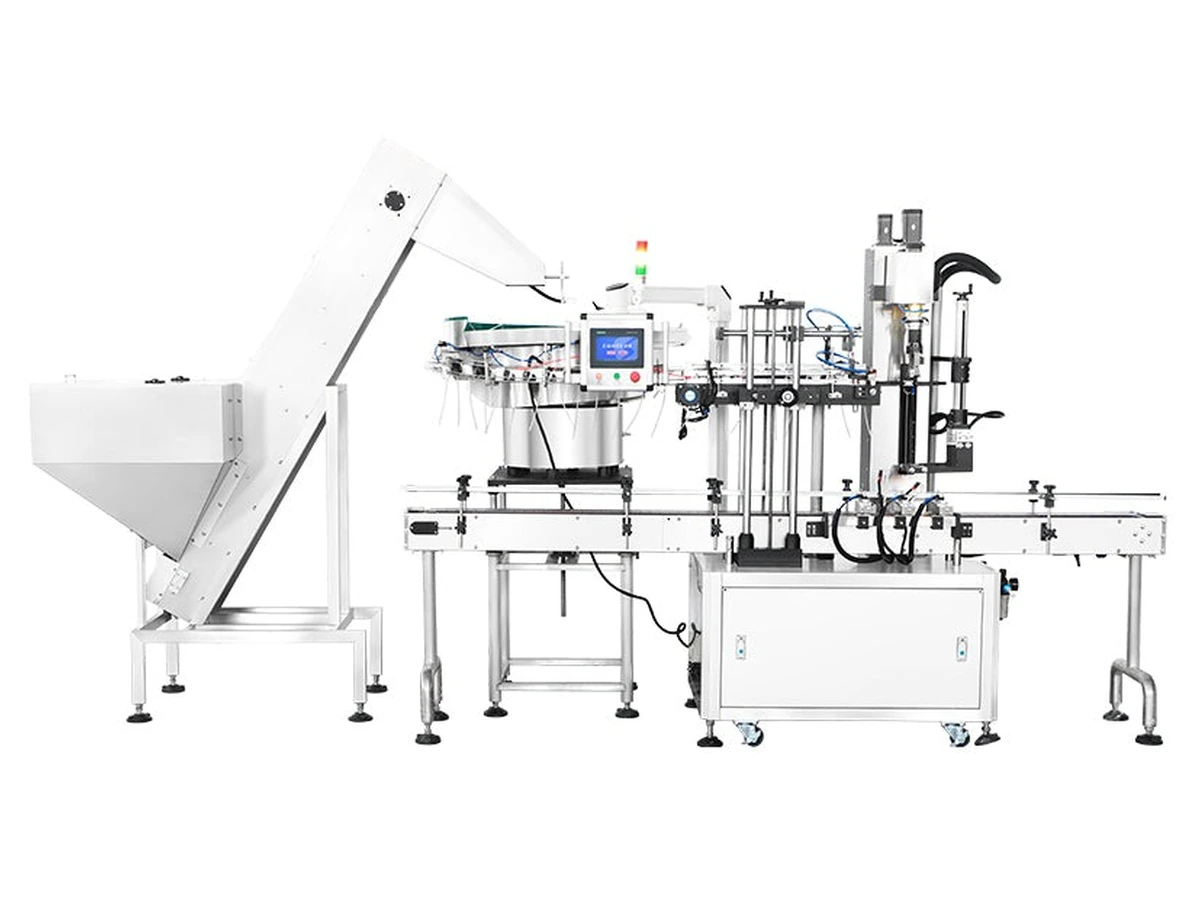
Automatic capping route for cleaning, home-care and chemical bottles with trigger sprayers.
View machine →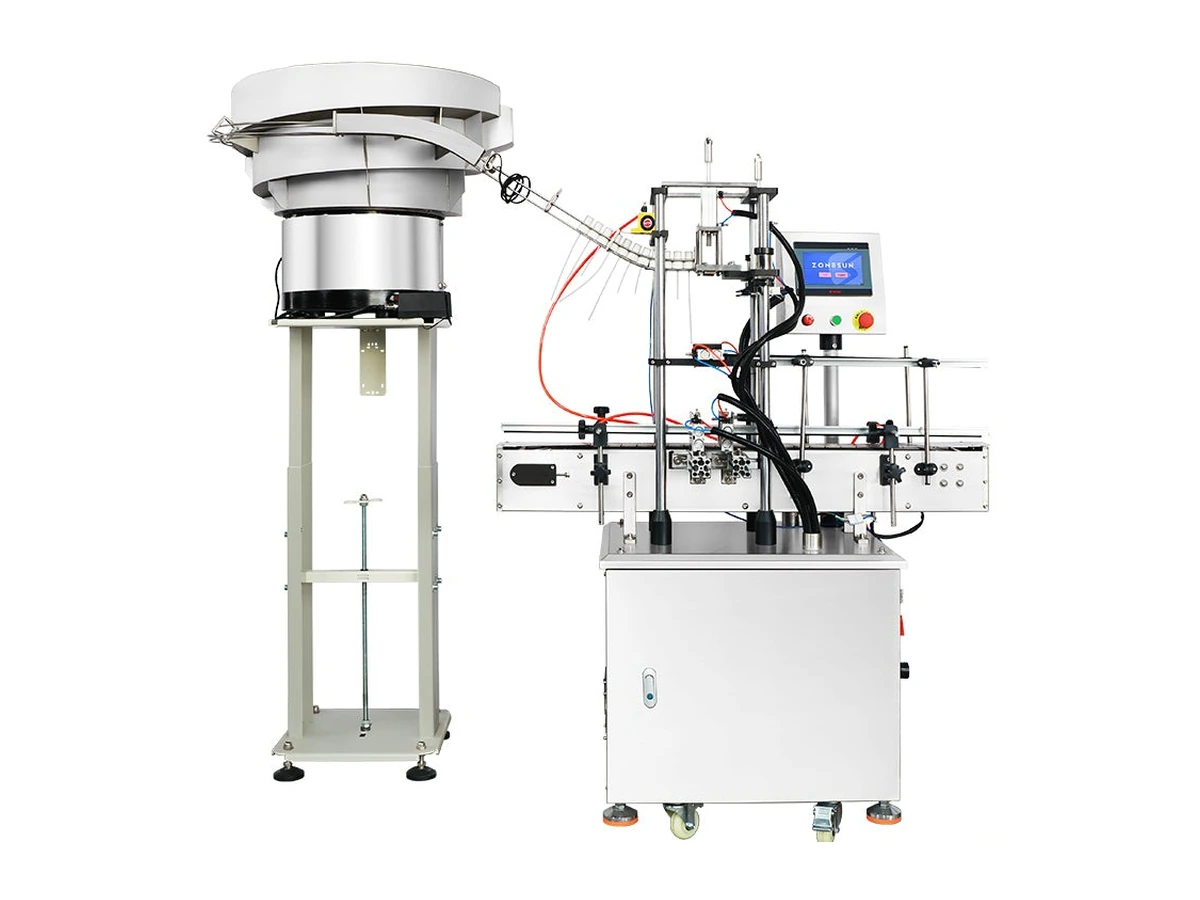
Feeding and orientation route for trigger sprayers with soft dip tubes.
View machine →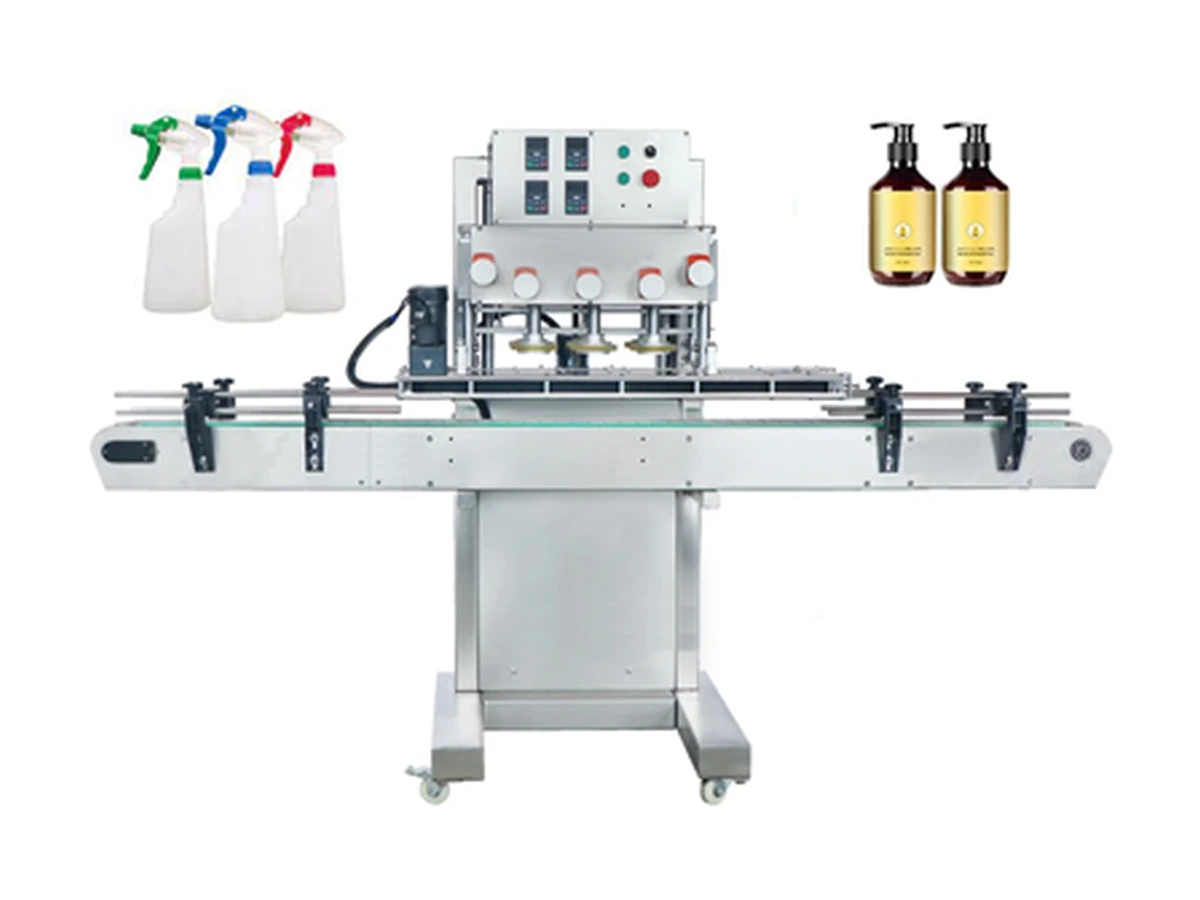
High-output inline belt and spindle capping route for compatible screw and spray closures.
View machine →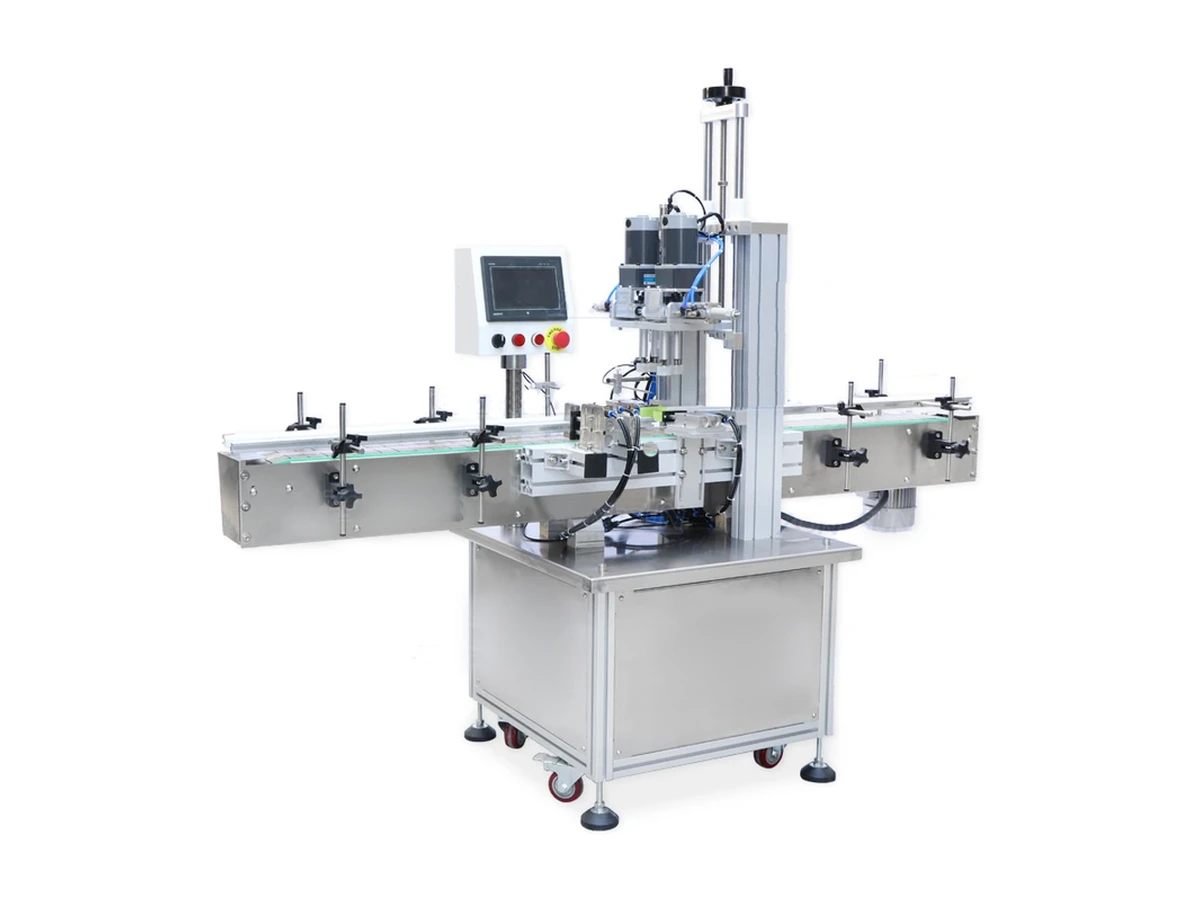
Automatic screw capping route for repeatable cap placement, torque and line integration.
View machine →Quick answers
Send bottle samples, trigger cap samples, tube length, product type, output target and line layout information.
Yes. Lancing can help compare manual-assisted, semi-automatic, compact and automatic trigger capping routes.
Yes. Filling speed, conveyors, labelling and pack-off can all affect the best capping-machine route.
Send bottle samples, trigger caps, dip-tube length, product details and target output. Lancing can help compare semi-automatic, compact and automatic routes.
More routes
Build the case for a trigger-capping change from recorded production work. Separate paid operator time, accepted output, rework and format changes so the same benefit is not counted twice. State the period observed and the product mix; one easy run should not stand for every planned batch.
Compare each proposed arrangement against that same baseline. Include the equipment and project items required to make it operational, then record any recurring costs that change. Keep assumptions about future demand, staffing and quality improvements separate from measured results so they can be challenged individually.
Only demand and a complete production plan can support that assumption; separate potential capacity from evidenced commercial benefit.
No. Show its inputs, exclusions and uncertainties so the business can assess the result on its own evidence.